Alfa Laval’s MaxiLobe Rotary Lobe Pumps boost efficiency, uptime, and lower TCO
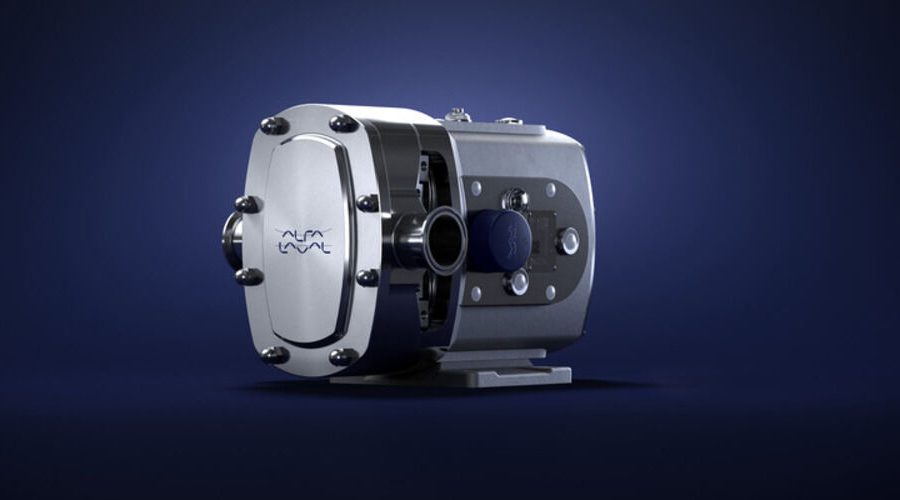
Alfa Laval has introduced its new MaxiLobe rotary lobe pump range, a next-generation positive displacement pumping solution engineered to enhance volumetric efficiency, cut energy consumption, and lower the total cost of ownership for manufacturers across the dairy, food and beverage industries.
Designed to tackle the rigorous demands of modern hygienic processing, the MaxiLobe series offers a broader operating envelope and superior reliability, helping industrial plants maximise operational uptime while protecting sensitive product quality.
Capital optimisation and retrofit simplicity
A central advantage of the MaxiLobe series is its high volumetric efficiency, which allows processors to deploy a smaller pump size for the same required duty in suitable applications. This right-sizing capability reduces capital expenditures on both equipment and associated electrical infrastructure.
Upgrading existing processing lines is equally straightforward. MaxiLobe is engineered with key porting dimensions that match legacy Alfa Laval SRU pumps and most SX and SX UltraPure models, enabling drop-in replacements without requiring costly pipework modifications. Under defined operating conditions, MaxiLobe delivers at least 5% higher flow rates than equivalent SRU models, boosting line capacity without increasing the equipment footprint.
Energy savings and shear protection
Maintaining product integrity while driving high-speed production is a constant challenge for food, dairy, and beverage manufacturers handling shear-sensitive fluids.
Because MaxiLobe pumps achieve target flow rates at lower rotational speeds, they drastically reduce fluid shear, safeguarding the texture and structure of delicate products. Operating at these reduced speeds also translates into significant energy savings, cutting electricity consumption by more than 25% in many standard applications. Furthermore, lower mechanical stress and a robust gearbox design combine to minimise unplanned stoppages, extend service intervals, and prolong overall equipment life.
Hygienic standards and easy maintenance
Hygiene, traceability, and food safety are non-negotiable in liquid food and beverage processing. The MaxiLobe series features precision-profiled elastomers and superior cleanability, carrying EHEDG and 3-A certifications alongside full FDA compliance as standard. For highly regulated pharmaceutical and biotech applications, the companion MaxiLobe UltraPure model complies with ASME BPE standards, cGMP guidelines, and USP requirements, backed by comprehensive Alfa Laval Q-doc documentation.
To minimise maintenance overhead, MaxiLobe is designed for quick, predictable servicing. It features front-loading single seals that can be replaced directly in-line without removing the pump from the process pipework, cutting routine downtime. Interchangeable components and accessible shimming further simplify upkeep.
Industry validation
“For decades, our rotary lobe pumps have been widely used in hygienic and high-purity processing where reliability and predictable performance are essential,” said Russ Kelly, portfolio manager, pumps at Alfa Laval. “MaxiLobe builds on that legacy with improved hygienic design across a wider operating range, enabling smaller pumps to achieve the same duty at lower speeds. Lower speeds reduce shear, helping improve operating efficiency and safeguard shear-sensitive products.”
Every MaxiLobe pump undergoes strict factory testing and is supplied with an individual performance certificate verifying compliance with its specified operating curve prior to delivery, ensuring smooth, reliable commissioning on the factory floor.